CNC bending is a sheet metal process in which a computer controlled press brake bends metal to a precise, programmed angle. Because each bend is programmed rather than set by hand, it repeats accurately across a whole run of parts, which matters wherever a project needs identical metalwork at volume.
At a glance
- CNC stands for computer numerical control. In sheet metal work, it means a press brake run from a programmed digital file.
- The three main bend types are air bending, bottoming and coining.
- The bending programme is built from the same CAD drawing used for cutting and fabrication.
- The first part off a run is measured against the drawing before the full run goes ahead.
- Mild steel, stainless steel and aluminium are all commonly CNC bent.
What is CNC bending?
CNC bending is the use of a press brake controlled by a programmed digital file to bend sheet metal along a straight line between a punch and a matching die.
An operator loads the sheet and starts the programme, and the machine carries out the bend sequence and angles exactly as set. Once a bend is programmed, it can be repeated identically across as many parts as the run needs. This is how our CNC bending and forming service produces matching parts across a whole run.
The programme is built from the same CAD drawing used earlier in the project, so the dimensions used for bending match the dimensions used for laser cutting and fabrication.
What are the main types of CNC bend?
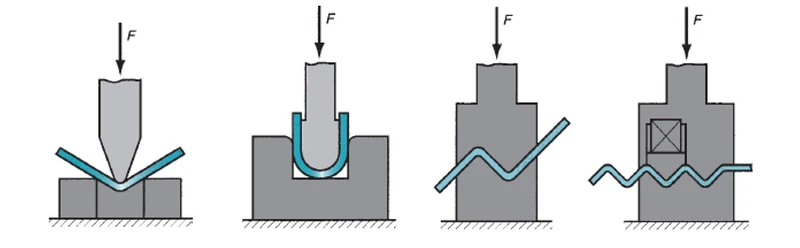
The three bend types used most in sheet metal work are air bending, bottoming and coining, and each trades flexibility for precision in a different way.
| Bend type | How it works | Best for |
|---|---|---|
| Air bending | The punch presses partway into the die, and the final angle is set by how far the punch travels | Flexibility: one tool setup produces a range of angles |
| Bottoming | The punch presses the material fully into the die | A sharper, more fixed angle with less variation |
| Coining | Much greater pressure is applied to the material in the die | A very precise angle, with springback largely eliminated |
The right choice depends on the material, the angle required and how much precision the design calls for.
How does a design become a programmed bend?
A CAD drawing is translated into a bending programme that sets every fold before the first part is made.
- The CAD drawing is converted into a bending programme.
- The programme sets each fold: its angle, its position along the sheet and the order of the bends, since an earlier bend can block access for a later one.
- The first part is produced and measured against the original drawing.
- The full run goes ahead once the first part matches.
How is quality checked across a run?
The first part off a run is measured against the drawing, and further parts are checked at intervals through a longer run.
These checks confirm the machine and the material are behaving as expected. The difference from manual bending is not that checking disappears, but that every part starts from a far more consistent baseline.
CNC bending vs manual bending
CNC bending programmes each bend once and repeats it exactly, while manual bending relies on an operator repeating the same judgement on every part.
| Manual bending | CNC bending | |
|---|---|---|
| How the angle is set | Judged by the operator, by eye and experience | Programmed once and executed by the machine |
| Consistency across a run | Depends on the operator repeating the same judgement, which gets harder on long runs | Every part is formed the same way |
| Rejected parts | More likely as a run gets longer | Fewer parts rejected for inconsistency |
| Speed | Each part is set and checked individually | Faster once the programme is set, especially on long or repeat runs |
Skilled manual work can produce excellent results. The advantage of CNC is that consistency no longer depends on one person getting the same call right every time.
Which materials can be CNC bent?
CNC bending works with the sheet metals used throughout construction and fabrication.
- Mild steel
- Stainless steel
- Aluminium
Each material springs back slightly after bending, by a different amount. That springback is accounted for in the programme, which is why a programmed process gives more predictable results than judgement alone. Thicker gauges need more force from the press brake and more care in planning the bend sequence, which is also set in the programme rather than decided on the day.
Where is CNC bent metal used in construction?
CNC bent sheet metal is used wherever a building repeats the same metal part across many units.
- Balustrade panels and infill
- Staircase stringers
- Cladding trims and flashings
- Brackets, fixings and fixing plates
- Gate and fence panels that must match from one unit to the next
- Internal brackets and structural trims that are never seen once installed
Where a design repeats across a building rather than being made once, CNC bending is the more practical route, because the cost of programming a bend is spread across every part the programme produces.
Why does consistency matter on a development?
Consistent parts prevent avoidable snagging on site, and that is what makes CNC bending valuable on a build programme.
- Less snagging: parts that vary slightly cause fitting problems, often when the programme is already tight.
- Faster changes: when quantities change, a floor is added to a phase or a design tweak applies to the remaining units, an existing programme can be reused or adjusted quickly.
- Predictable planning: output for a repeat run is far easier to forecast than work that depends on manual judgement across dozens or hundreds of parts.
How Accents & Art handles CNC bending
At Accents & Art, CNC bending sits inside one in-house process that runs from concept and CAD design through welding and fabrication, finishing and installation, in our workshop in Accra, Ghana.
One team carries the specification from the drawing to finished, fitted metalwork, rather than passing it between separate suppliers. The fewer handoffs a specification goes through, the fewer chances it has to drift, and you have one party accountable for the result.
Frequently asked questions
What does CNC stand for in CNC bending?
CNC stands for computer numerical control. In CNC bending, a press brake follows a programmed digital file to set the angle, position and order of each bend, rather than being adjusted by hand for every part.
What is springback in sheet metal bending?
Springback is the tendency of metal to spring back slightly after it has been bent. In CNC bending it is accounted for in the programme, and coining applies enough pressure to largely eliminate it.
Is CNC bending better than manual bending?
For repeated parts, yes. CNC bending forms every part in a run the same way, which means fewer rejects and a faster process once the programme is set. Skilled manual bending can still produce excellent one-off results.
What should I ask a fabrication partner about CNC bending?
Ask how a specification moves from drawing to finished part, and whether design, fabrication and installation sit with one team or are split across several suppliers. Fewer handoffs mean fewer chances for the specification to drift.
If your project needs metalwork produced consistently across multiple units, start a commission and tell us what your build programme needs.